
The problem—suppliers that don’t speak the same language
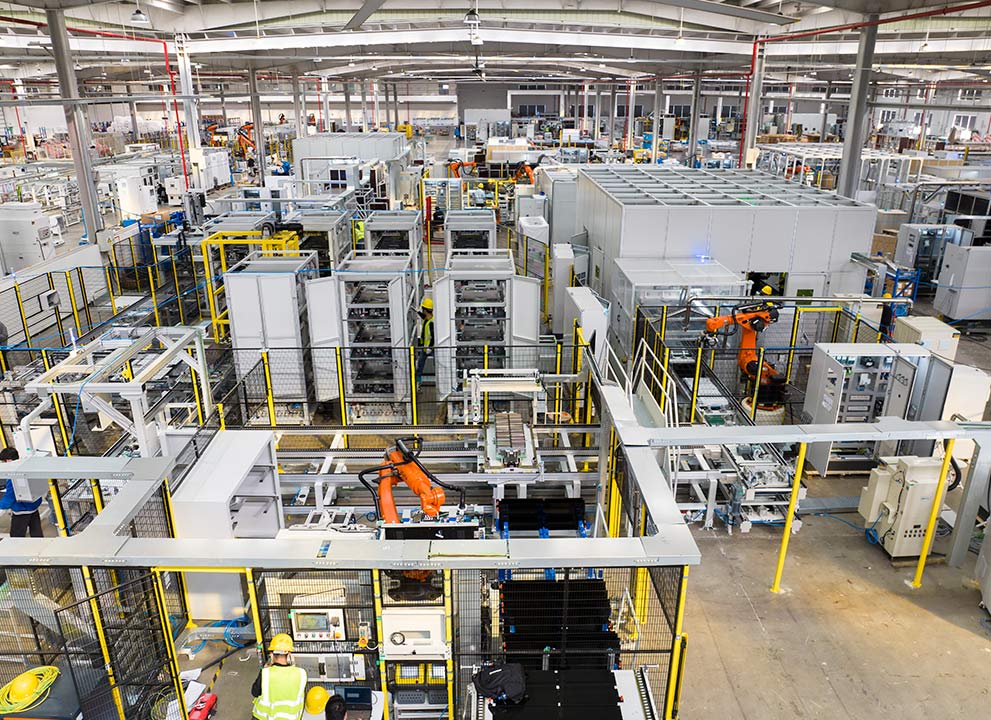
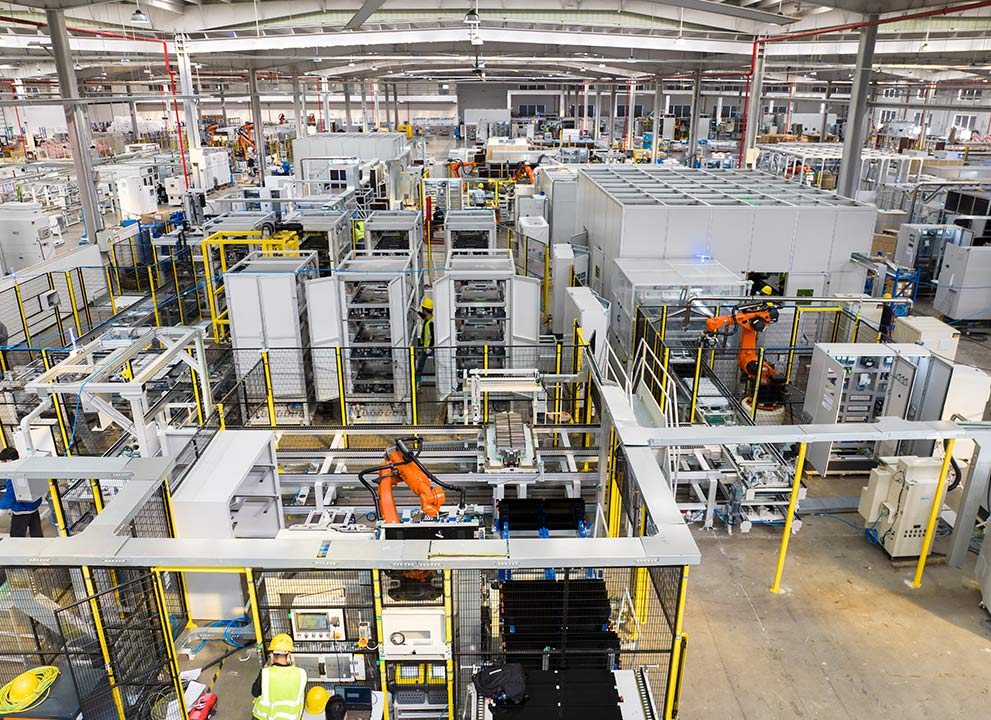
If you prefer surprises on your balance sheet, feel free to leave cell vendors, module builders and test houses to their own devices. For the rest of us who enjoy repeatable outcomes, the immediate problem is mismatched expectations across functions. I’ve seen lines where automation was treated like a suggestion; that’s why modern projects reference battery manufacturing automation early and often. Real production realities matter—think Guangdong province, China—because physical layout, logistics and regulatory touchpoints change choices on the floor. Effective integration demands clear handoffs between cell assembly, module production and final pack testing, and it demands precisely described acceptance criteria for each handoff. You should also read manufacturer guidance for Battery Production when aligning test specs with supplier capabilities.
Root causes you must address immediately
– Misaligned tolerances: mechanical and electrical tolerances get negotiated away until failure appears on test logs. – Hidden process variance: suppliers use different recipes for electrode handling, thermal control and curing without sharing control charts. – Test blind spots: module tests that don’t reproduce pack thermal and mechanical stresses. – Communication drift: contract language that promises “compatibility” but defines nothing measurable. Tackle the first two lines. They create the rest.
A practical checklist for integration
– Define measurable acceptance: voltage, resistance, thermal map, mechanical deflection, and acceptable rework rates. State units and test fixtures. – Establish physical and data interfaces: connector pinouts, harness lengths, file formats from testers, and cadence for telemetry. – Agree on sample plans: lot size, destructive vs non-destructive sampling, and failure thresholds that trigger containment. – Lock down change control: any recipe, jig or algorithm change requires a signed protocol and regression check. – Assign a single technical owner per interface to resolve disputes within 48 hours. These items replace polite assumptions with obligations.
Testing strategy that exposes real risk
Run sequence-based stress tests that combine electrical, thermal and vibration inputs. Single-mode tests (only charge/discharge, only thermal cycling) are comforting; they don’t reflect installation reality. Make sure test protocols include: – Combined soak-and-cycle routines to detect latent interconnect failures. – Module-to-pack integration tests that exercise busbar dynamics. – Field-data replay using logged duty cycles from comparable vehicles or stationary systems. Document test rigs and software versions. If a supplier’s test stand can’t reproduce pack-level faults, it doesn’t count.
Common pitfalls and how to avoid them
– Relying on vendor-supplied validation without independent checks: request raw data and audit access. – Over-optimistic cycle life claims: ask for statistical test plans, not glossy charts. – Treating software updates as background maintenance: firmware alters safety margins; treat updates like hardware changes. – Ignoring logistics: damage during transport will masquerade as manufacturing defects. Include transport simulation in early trials. Cure each with documented requirements and at least one third-party verification step.
Comparing supplier models—who to trust for what
– Full-service pack integrators: choose them when you want turnkey responsibility and predictable boards on invoices. Expect less direct control. – Component specialists (cell or module only): use them when you need technical depth on a particular process, but plan for integration cost. – Specialized test houses: bring them in for objective validation when your teams and suppliers disagree. Evaluate using the same scorecard: technical capability, traceability systems, flexibility to follow your change control, and real sample reports from recent projects.
Implementation steps with minimal drama
1) Lock acceptance criteria and sampling plans before the first purchase order. 2) Run a pre-production pilot that stitches one cell supplier, one module supplier and one test path together. Fail fast and fix. 3) Formalize corrective action timelines and responsibilities. 4) Put data sharing agreements in place so test logs move with the hardware. 5) Move to serial production only after a statistically meaningful pilot and an agreed containment plan. Speed without checkpoints creates rework. Discipline yields fewer surprises.

Closing synthesis
You can be politely astonished when integration fails, or you can design for clear, measurable handoffs and enforce them. My advice comes from years auditing assembly and test sequences and from negotiating the awkward moments when a cell behaves differently in a pack than in isolation. Practical steps—measurable acceptance, combined testing, signed change control, and honest vendor comparisons—remove ambiguity. For projects that need an experienced partner to translate requirements into shop-floor practice, FHS provides procedural rigor without theatrical promises, delivering the technical alignment you actually need.